
 English
 русский
Tungsten Carbide Cutting Blades: Grades, Types, Uses, and How to Choose
Industry News-If you spend your working hours in front of a lathe or a machining center, the tungsten carbide cutting blade is probably the most consequential consumable in the tool crib. It decides how fast the machine can run, how often someone stops to index an edge, and whether the last part in a batch measures as cleanly as the first. Yet blades are often chosen by habit — "this is what we have always used" — rather than by matching a grade and a geometry to the material and the machine.
This guide is for the people who actually make chips: machinists, process engineers, tooling buyers, and shop owners chasing predictable results in hard materials. We will look at what tungsten carbide is, how a blade is built, where different types earn their keep, and how to choose and care for them.
Content
What Makes Tungsten Carbide So Good at Cutting
Tungsten carbide is not a metal in the ordinary sense. It is a composite made by pressing and sintering tungsten carbide grains with a metallic binder, most often cobalt. The grains provide the hardness; the binder holds them together and gives just enough toughness to survive a real cut. Tuning that balance is the whole art of carbide manufacturing.
Hardness That Survives Heat
Hardness alone is easy to find — plenty of steels are hard at room temperature. The interesting question is what happens when the edge heats up. High-speed steel starts to soften at temperatures that occur routinely in a cut, which is why HSS tools slow down, wear quickly, and need frequent regrinding. Carbide holds its hardness much further up the temperature scale, so you can push surface speed and feed harder and still find a sharp edge when you look at the tool.
Wear Resistance, With One Honest Trade-Off
Carbide also resists abrasive wear exceptionally well, which keeps a blade cutting steadily instead of rubbing and work-hardening the workpiece. The trade-off is brittleness: a carbide edge does not like vibration, loose setups, or a worn tool holder. Treat it well and it outlasts steel by a wide margin; treat it badly and it chips, and no grade on the market will save it.
The Anatomy of a Tungsten Carbide Cutting Blade
When people talk about a carbide blade, they are usually describing the end result of four decisions: the grade, the geometry, the edge preparation, and the coating. Getting three right and one wrong is a common reason a tool underperforms.
Grades and Binder Content
Grades are described by grain size and cobalt content. Coarse grains with more binder give toughness for roughing and interrupted cuts; fine grains with less binder give hardness and edge retention for finishing. Most suppliers sort grades into the standard ISO colour groups, and it helps to know which group you are standing in when you open the tool cabinet.
| Class | Workpiece group | What it is generally used for |
|---|---|---|
| P | Steel | Turning, milling and boring of carbon and alloy steels |
| M | Stainless and high-alloy steel | Cuts where built-up edge and work hardening are a risk |
| K | Cast iron and non-ferrous | Short, broken chips and abrasive workpiece surfaces |
| N | Aluminium and non-ferrous metals | High-speed cutting where a sharp, polished edge matters |
| H | Hardened steel | Light finishing cuts on very hard materials |
Geometry, Edge Prep, and Coatings
Geometry decides how the chip forms and where the heat goes. A positive rake cuts freely and is gentle on slender parts; a negative rake puts more material behind the edge and stands up to heavy interruption. Edge preparation — a light hone or a small T-land — stops a freshly ground edge from chipping the moment it touches the workpiece. Coatings reduce friction and heat at the cutting zone. They are a real advantage in continuous cutting, but they are not a substitute for a stable setup.
Where These Blades Go to Work
Carbide cutting blades are a family built around one material and adapted to different operations. Common jobs include:
- Turning and facing shafts, hubs, and hydraulic components
- Milling flats, shoulders, and slots on steel and cast iron parts
- Grooving, parting off, and thread turning where a narrow, stable edge matters
- Boring and internal finishing where chatter is the constant enemy
- Finishing cuts on hardened or heat-treated components
- Machining aluminium, brass, and composite parts at high spindle speeds
The workpiece matters as much as the operation. Mild steel and cast iron are forgiving; stainless steels work-harden under a dull edge; aluminium rewards a sharp, polished geometry. When a blade fails early, the cause is usually a mismatch between one of those conditions and the tool.
Choosing the Right Blade: A Short Checklist
Before reaching for a catalogue, answer a few questions about the job. The answers narrow the field faster than any specification table.
- What material are you cutting, and in what condition — annealed, normalized, hardened, or cast?
- What operation is it: continuous turning, interrupted milling, parting, grooving, or threading?
- How rigid is the setup, and how much overhang does the holder actually have?
- Can the machine deliver the speed and feed the grade needs, with coolant where required?
- Does the job call for roughing volume, or for a controlled finish and tolerance?
- What does stopping the machine cost, compared with the price of a better blade?
If you want a closer look at the common blade types and how each is used, our team keeps a guide to blade types, uses, and selection on the site that goes deeper into the geometry side.
Keeping an Edge Alive on the Shop Floor
Most blade failures announce themselves before they become scrap. Learning to read the wear pattern is the quickest way to add tool life without spending anything.
| Symptom | Usual cause | First thing to check |
|---|---|---|
| Chipping along the edge | Vibration or an interrupted cut | Rigidity, overhang and clamping |
| Cratering on the rake face | Cutting temperature too high | Speed, feed and coolant delivery |
| Built-up edge | Speed too low for the material | Surface speed and coating choice |
| Fast flank wear | Abrasive workpiece or wrong grade | Grade class and workpiece hardness |
| Poor surface finish | Dull edge or unstable setup | Edge condition and tool seating |
A blade that indexes too often is rarely fixed by buying a cheaper blade. It is usually fixed by correcting one of three things: the setup, the cutting data, or the grade.
Thirty Years of Carbide, and One Practical Focus
We are Jiangsu Gaite Tungsten Technology, a carbide manufacturer based in Changzhou, in the south of Jiangsu Province. The company started in 1990 and moved into cemented carbide around the turn of the century, bringing in experienced technical people and the equipment needed to press, sinter, and grind hard material properly. In 2009 we added a low-pressure sintering furnace and a TPA press, which let us control density and structure from the powder stage rather than buying in blanks. Later investments included grinding and measurement equipment from Germany, a five-axis tool grinder, and a digital tool presetter from Sweden.
That progression shapes how we think about blades. We make tungsten carbide cutting blades for metal cutting work, and we also produce inserts and wear parts for tunnel boring machines, road milling, rock drilling, coal mining, and stamping dies. The same material science runs through all of it, so a problem on a milling insert often teaches us something useful about a rock drilling bit. We work to ISO9001 and ISO14001 certified processes from powder to finished edge.
 Tungsten Carbide Cutting Blade with GR6X-A and GR6C-A GradesTungsten carbide cutting blade for metal cutting, with GR6X-A and GR6C-A grades for cast iron, steel, and nonferrous finishing or semi-finishing.View Product →
What we hear most from customers is not that they need something exotic. They need a blade that behaves the same way on Monday morning as it did on Friday afternoon — the same grade, the same geometry, batch after batch. That consistency, plus a willingness to look at a drawing or a worn tool and work out what the job actually needs, is what we try to offer.
The Short Version
A tungsten carbide cutting blade is a small, affordable part with an outsized effect on productivity. Choose the grade for the workpiece, the geometry for the operation, and the edge preparation for the stability of your setup. Keep the holder rigid, keep the cutting data sensible, and change the edge before it fails rather than after. Do that, and the blade will quietly do what it was bought for.
If you are working through a specific application and want a second opinion on grade or geometry, our team is glad to look at the details with you.
Our Products //
Related Products
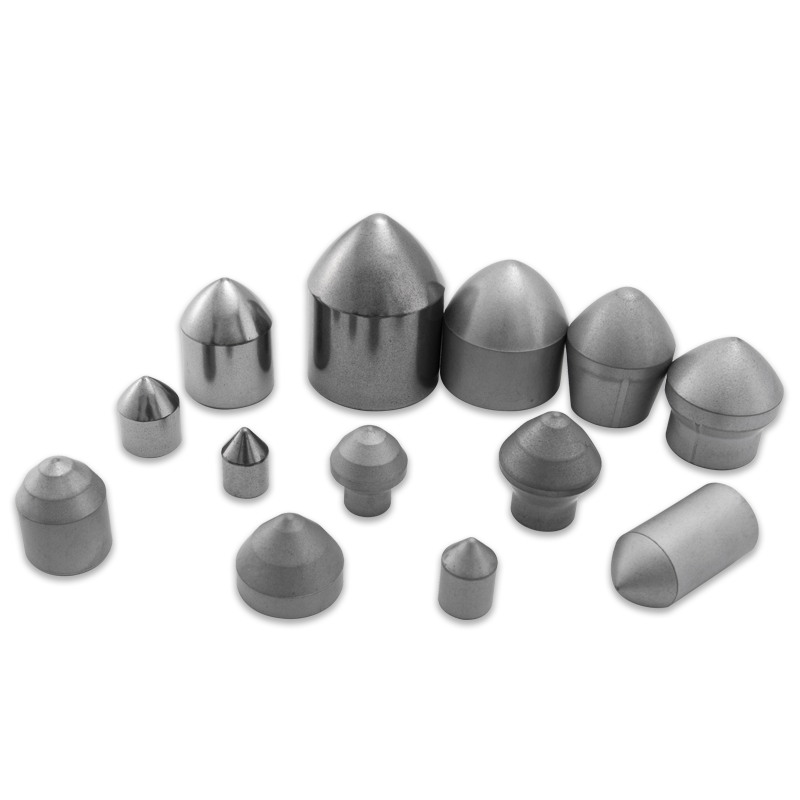
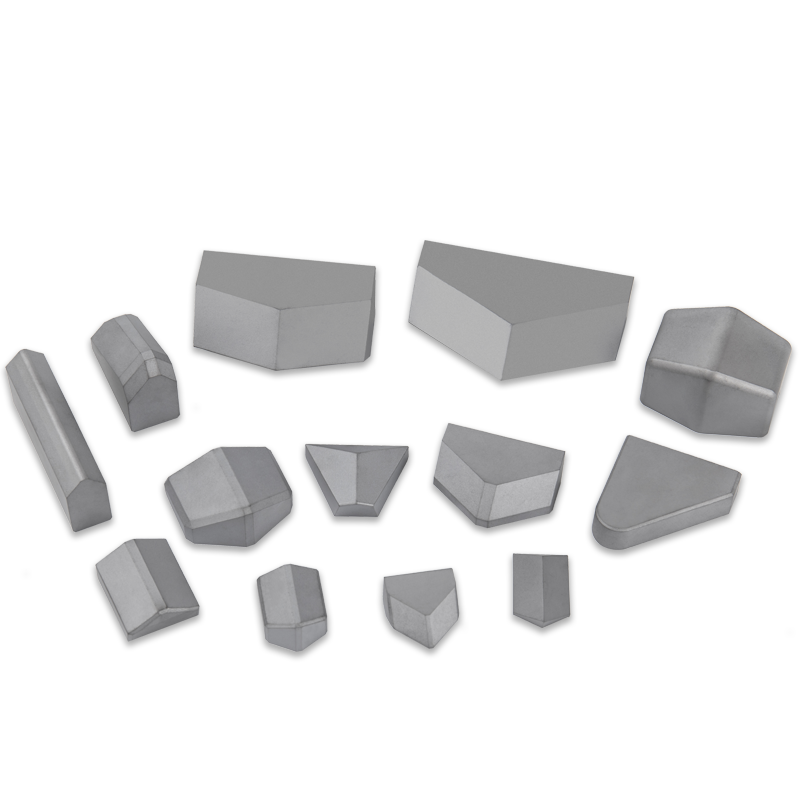
If you are interested in our products, please consult us
